

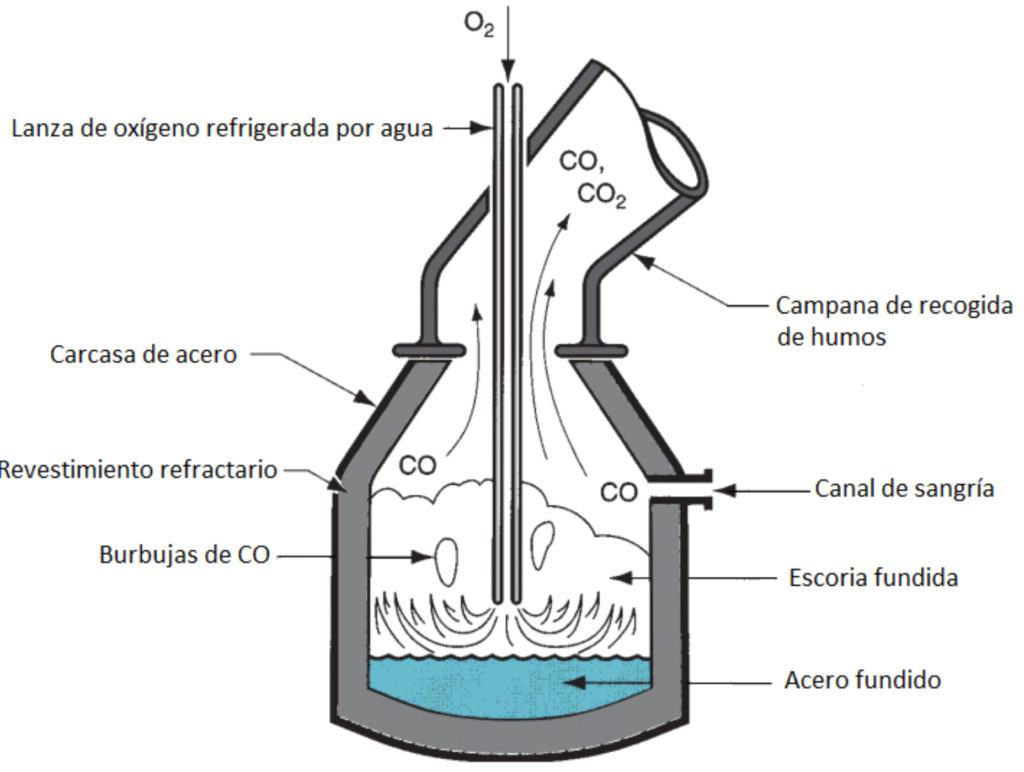
In a basic oxygen furnace, carbon-rich molten iron (pig iron) is converted to steel by blowing oxygen through a top-mounted lance at supersonic speeds into the molten iron. This reduces the carbon content of the alloy and converts it into low carbon steel.
Due to the high competitiveness of the industry, it is essential to achieve process control to ensure optimum efficiency, maximizing product quality and process safety and minimizing energy consumption.
Process
The oxidation of carbon during the oxygen conversion process is of vital importance to reduce the level of carbon and other impurities.
When oxygen is blown over the molten metal, as a result of the reaction, the temperature increases and a large amount of CO and CO2 gases are produced, causing agitation of the metal and slag.
Here the slag layer plays an important role in binding carbon and other impurities and helps to remove hydrogen, nitrogen and some of the non-metallic inclusions from the metal.
Therefore, monitoring CO concentration is a key indicator to determine when the melting process and decarbonization has reached its end point.
Measuring the O2 level helps the operator control the flow of oxygen to the melt.
Typical process data
O2 = 0 – 2 %
CO = 50 – 55 %.
CO2 = 10 – 20 %.
Temperature: 60 – 90°C
Pressure: atmospheric
Optical path length: 1 – 2.5 meters
Target
Accurate measurements to track the decarbonization process, maximize product quality, minimize energy consumption to maintain process control in the oxygen feed.
- Optimize oxygen consumption
- Improved product quality
- Improved process control to determine the end point of the melting process
- Improved safety
- Increased productivity
Our solution
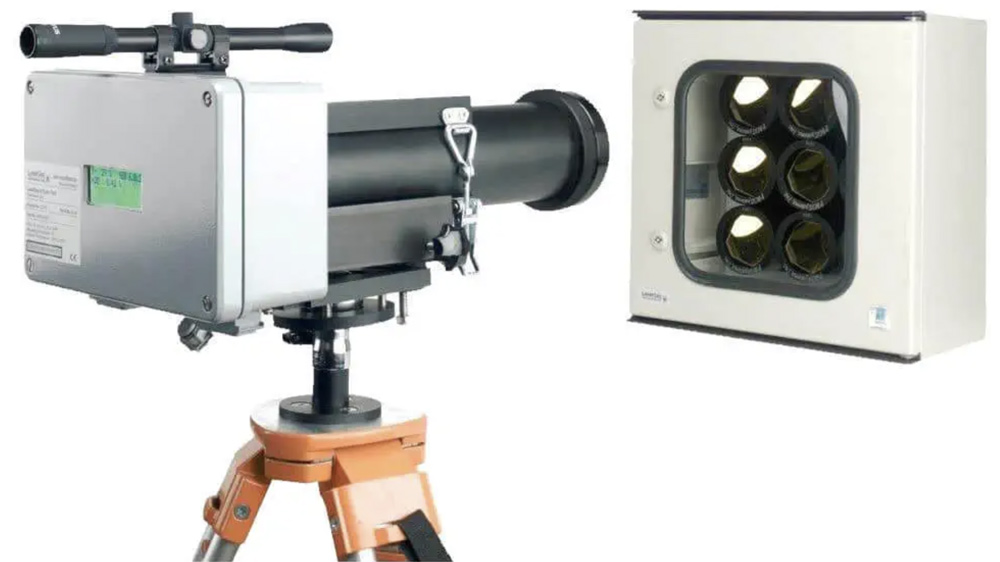
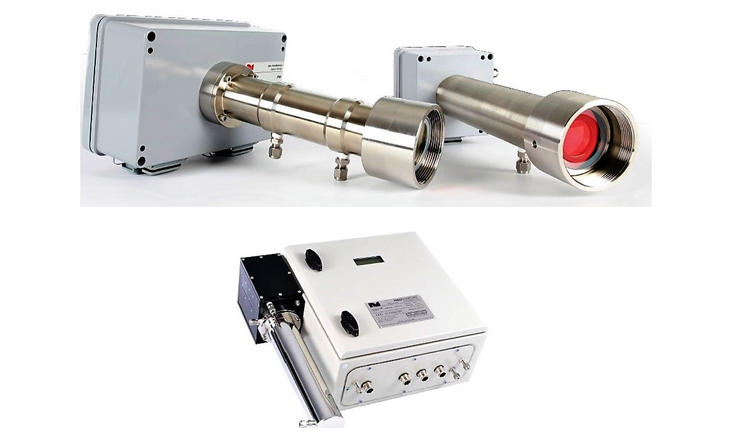
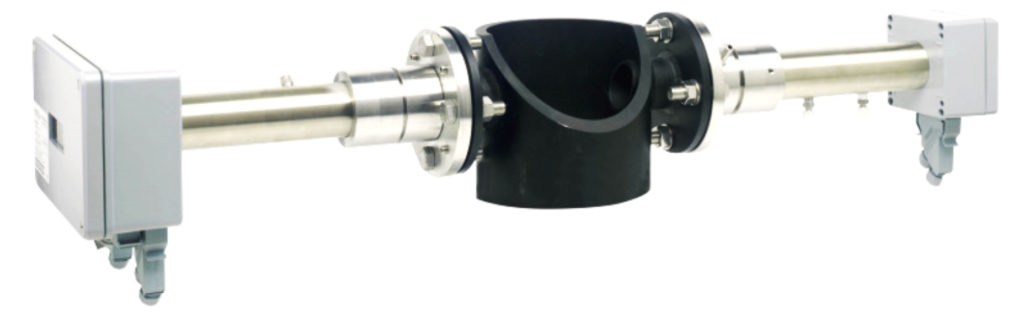
Norway-based NEO Monitors’ LaserGas™ II SP is a well-proven analyzer in the steel industry and is the right solution for optimized process control. State-of-the-art design and innovative functionality ensure that the instrument delivers
unmatched reliability and durability in a compact solution.
LaserGas™ II SP
- Measure directly in the process (In-Situ)
- Long service life
- No need for sampling systems
- Fast response time (typical 5s)
- Low maintenance cost
- Standard configuration O2 and CO
- ATEX/IECEx Zone 1 & 2, CSA Class 1 & 2
Benefits
- High sensitivity
- Proven measurement technology
- No consumables
- Highly reliable
- Easy to install and operate
For more information contact MATELCO, SA at comercial@matelco.es.